
Processing
Constructive process
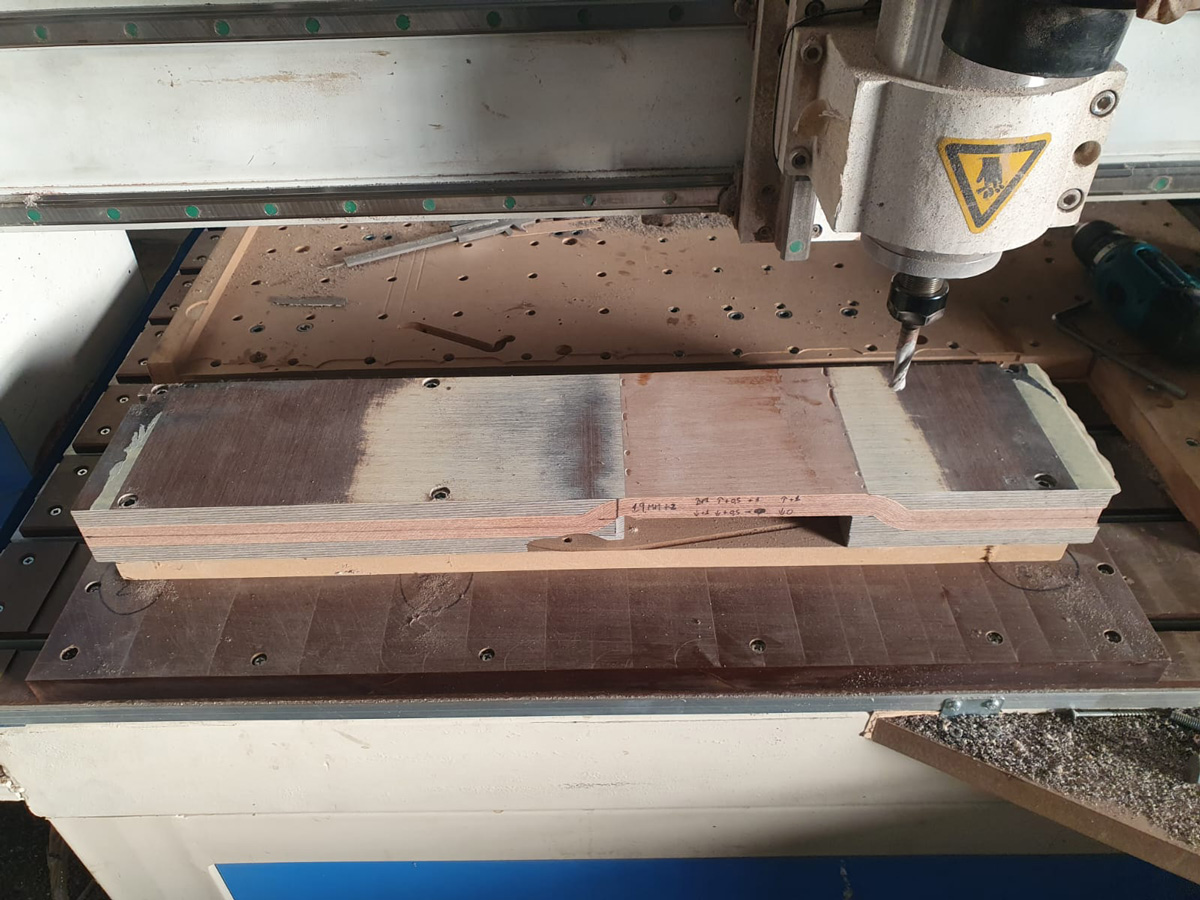
The idea of this new procedure comes from the fact of wanting to create a central core, which we will call core, with uninterrupted veins, so as to have an extremely stable arc and with 0 front twist during the traction phase. The "core" is formed by various layers of wood 0.6 mm thick suitably crossed to 45# in the necessary areas, glued, with special resins, in the matrix (mold and counter mold) and crushed at very high pressure (10 kg/ cmq).
The product is left to rest in the press for about 24 hours, after which the slow cooking always under pressure begins, the timing varies from external temperatures, however never lower than 24 hours between heating, resin stabilization, cooling. This process produces a fully stabilized densified conglomerate with relative humidity below 2%.
The second part of the process involves the addition of lateral thicknesses, in the necessary parts, (which we will call plaques). These can be made of various essences, from solid wood, to the pre-component industrial treated with melamine glues, to the Rexilon preset (stratified stabilized with phenol-resorcine glues), to the pre-component stratified densified with fiber angle 90.
The latter, the most laborious and expensive, can be requested with colors chosen by the customer, except for the feasibility of procurement. The pre-set densified, of our production, requires the same processing of the "core", then bonding of the various layers of 0.6 mm high pressure molding, 24 H rest and 24 H.
Once the wooden "plates" are made, a process is carried out in a calibration machine, then subsequently a further processing to give it the correct shape to fit perfectly to the curves of the core. Once this process has been carried out, there is the phase of further gluing, between plates and cores.
In this case we use a specific adhesive with higher elastic characteristics and with higher density. Glued everything repeats the process of pressing and cooking (24 h + 24 h). At this point we have a raw wooden panel of larger dimensions than the future riser.
We move on to the squaring of the panel, final calibration, CNC positioning for a preliminary drilling, which will serve us to make the subsequent placements. Once we have the drilled product you go to place and tighten in the machine for the first CNC placement. This will be followed by another 6 before arriving at the final raw riser.
Now, depending on the model, the various bushings must be mounted and glued. Fitted the hardware, which will remain fixed in the riser, we move on to the sanding manual, to the adaptation of the grip and window plate ( uesti 2 steps determine the perfect calibration of the riser), to the fine sanding, to the painting phase
It is now time to mount all the necessary components, screws, pins ilf, grains, countergrains, screws tightening, any rest, calibration and alignment future bending.
Here is our fantastic riser, ready to be tried.



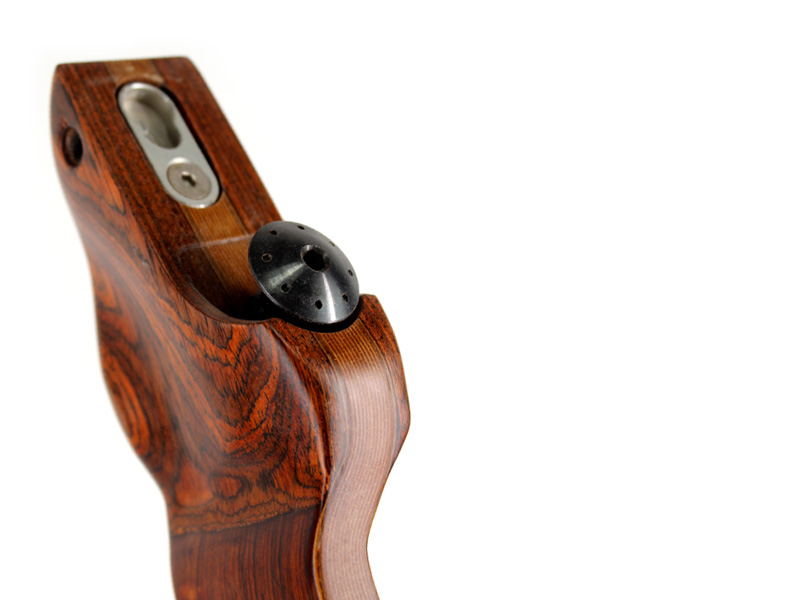
Riser 19 inch
These risers are perfectly within the parameters World Archery, Fitarco, Fidasc, Fiarc in the category "Traditional bow". Risers can also be equipped with internal weights to increase weight and stability (only in the construction phase). The side plates can be requested with colors of your choice.
Discover the various modelsRiser 21 inches
These risers are perfectly within the parameters World Archery, Fitarco, Fidasc, Fiarc in the category "Traditional bow". Risers can also be equipped with internal weights to increase weight and stability (only in the construction phase). The side plates can be requested with colors of your choice.
Discover the various models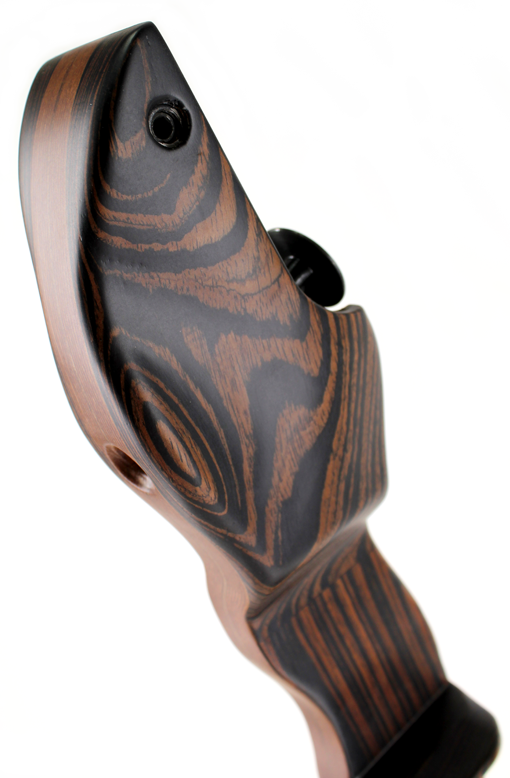

Riser 25 inch
Riser for 25 inch traditional Olympic bows. These risers fall perfectly within the World Archery, Fitarco, Fidasc, Fiarc parameters in the "Traditional Bow" category. The risers can also be equipped with internal weights to increase their weight and stability (only during the construction phase). The side plates can optionally be requested with colors of your choice.
Discover the various modelsWould you like more information about our risers?
Write to us now, we will reply as soon as possible.

Special thanks to:
Filippo Clini - Athlete of the Italian national team from 1990 to 2001. World Junior Champion 1991. World university champion 1997. 10 Italian titles. Italian national coach from 2004 to 2014, Olympic Silver medalist Beijing 2008. He helped high-level archers win world championships, European championships, stages and world cup finals. Author of the official texts for Fitarco training; Author of over 100 official publications and current reference technician for numerous professional athletes. World Archery Level 3 trainer, offers his collaboration in technical seminars and training camps all over the world.
It was fun collaborating with Denis and seeing such an innovative product come to life. A traditional riser but absolutely modern at the same time, which gives enormous pleasure to those who try it.
EliVanes, Shooting different ... Shooting for the Gold
For years EliVanes has been a consolidated reality in the global aeronautics sector, and our products are the result of careful studies, research on materials, laboratory tests, field trials, and everything else necessary to create something increasingly high-performance. Discover all the EliVanes models ideal for your arrow and dedicated to all types of archery.
